Overview
Automotive logistics is the planning, execution, and control of material and information flows involved in manufacturing, distributing, servicing, and recovering motor vehicles and their components. It spans inbound deliveries to suppliers and assembly plants, movement within plants, outbound distribution of finished vehicles, aftermarket parts fulfillment, and reverse logistics.
The discipline connects manufacturers, tiered suppliers, carriers, ports, warehouses, dealers, and repair networks. Its importance lies in coordinating high volumes of different parts with production schedules while controlling cost, inventory, damage, and disruption. Techniques such as cross-docking and warehouse inventory management support particular stages of these flows.
Etymology and Origins
The term combines automotive, relating to motor vehicles, with logistics, the coordination of complex operations and resources. The latter has a documented association with military supply and movement before its broader commercial use; see the dictionary history and definitions of logistics. No single first documented use of the combined phrase automotive logistics is established here.
As automobile production expanded, the terminology used to describe its material flows evolved alongside manufacturing methods. Concepts such as just-in-time production later became closely associated with supplying vehicle assembly operations.
Historical Development
- Early 1900s–1910s: Automobile production moved toward larger-scale, standardized manufacturing. Henry Ford’s moving assembly line began operating at the Highland Park plant on 1 December 1913, increasing the need to deliver compatible parts to workstations in a repeatable sequence; see The Henry Ford’s account of the assembly line and Britannica’s history of the automobile.
- 1940s–1970s: After the Second World War, Toyota developed the foundations of the Toyota Production System, including just-in-time and jidoka. Taiichi Ohno is closely associated with its development. Pull-based replenishment and small inventories shaped subsequent automotive material-flow practices; the system was refined over decades rather than introduced on a single date.
- 1970s–1990s: Computerized production planning and electronic information exchange increasingly supplemented paper schedules. The Automotive Industry Action Group (AIAG), founded in 1982, later became a forum for common automotive quality and supply-chain practices. Barcode identification expanded across industries after the first UPC retail scan in 1974, an important milestone in barcode history; automotive plants also used other symbologies. Ohno’s Toyota Production System, first published in Japanese in 1978 and in English in 1988 as Toyota Production System: Beyond Large-Scale Production, helped explain the production philosophy to a wider audience.
- 2000s–present: Enterprise systems, warehouse software, scanning, telematics, and automation have improved the ability to record and coordinate movements. RFID and analytics are used in selected applications, although adoption varies. The growth of electric vehicles has also increased attention to battery supply chains; the IEA’s Global EV Outlook 2024 documents the expansion of the market as of that report.
Core Concepts
Automotive logistics aligns physical flows with production and customer demand. A typical inbound process converts a plant schedule into supplier releases, arranges collection or delivery, receives and checks parts, and replenishes the correct line-side location. Purchase-order receiving and stock replenishment are examples of supporting warehouse processes.
Just-in-time (JIT) seeks to provide what is needed, when needed, and in the quantity needed, as described in Toyota’s account of the Toyota Production System. Just-in-sequence (JIS) adds the requirement that variant-specific components arrive in the order vehicles will be assembled. For example, seats for different vehicle configurations may be delivered in build sequence. JIS reduces line-side sorting but makes accurate sequencing and recovery from delays especially important. No single inventor or first-use date for JIS is established here.
Material may travel directly from a supplier, through a consolidation center, or on a milk run in which one vehicle collects from several suppliers. Returnable containers often circulate between facilities. Planners balance transport frequency and cost against inventory, available space, production risk, and delivery reliability.
Operational Flows and Applications
Inbound and plant logistics
Inbound teams coordinate raw materials, stamped parts, electronics, seats, tires, and other components from multiple supplier tiers. At the plant, receiving, storage, kitting, and line-side delivery make materials available for assembly. Kitting can group parts for an operation or order, while cross-docking can reduce storage time for suitable flows.
Illustrative JIS scenario: A plant changes its build order after a vehicle fails inspection. The logistics team must communicate the revised sequence, identify the affected seat racks, and verify their order before line-side delivery. A practical contingency is to define who can authorize resequencing and where mismatched parts will be held; this supports the Toyota Production System’s goal of providing needed items at the needed time. The scenario is illustrative, not a record of a specific plant event.
Finished vehicles and aftermarket parts
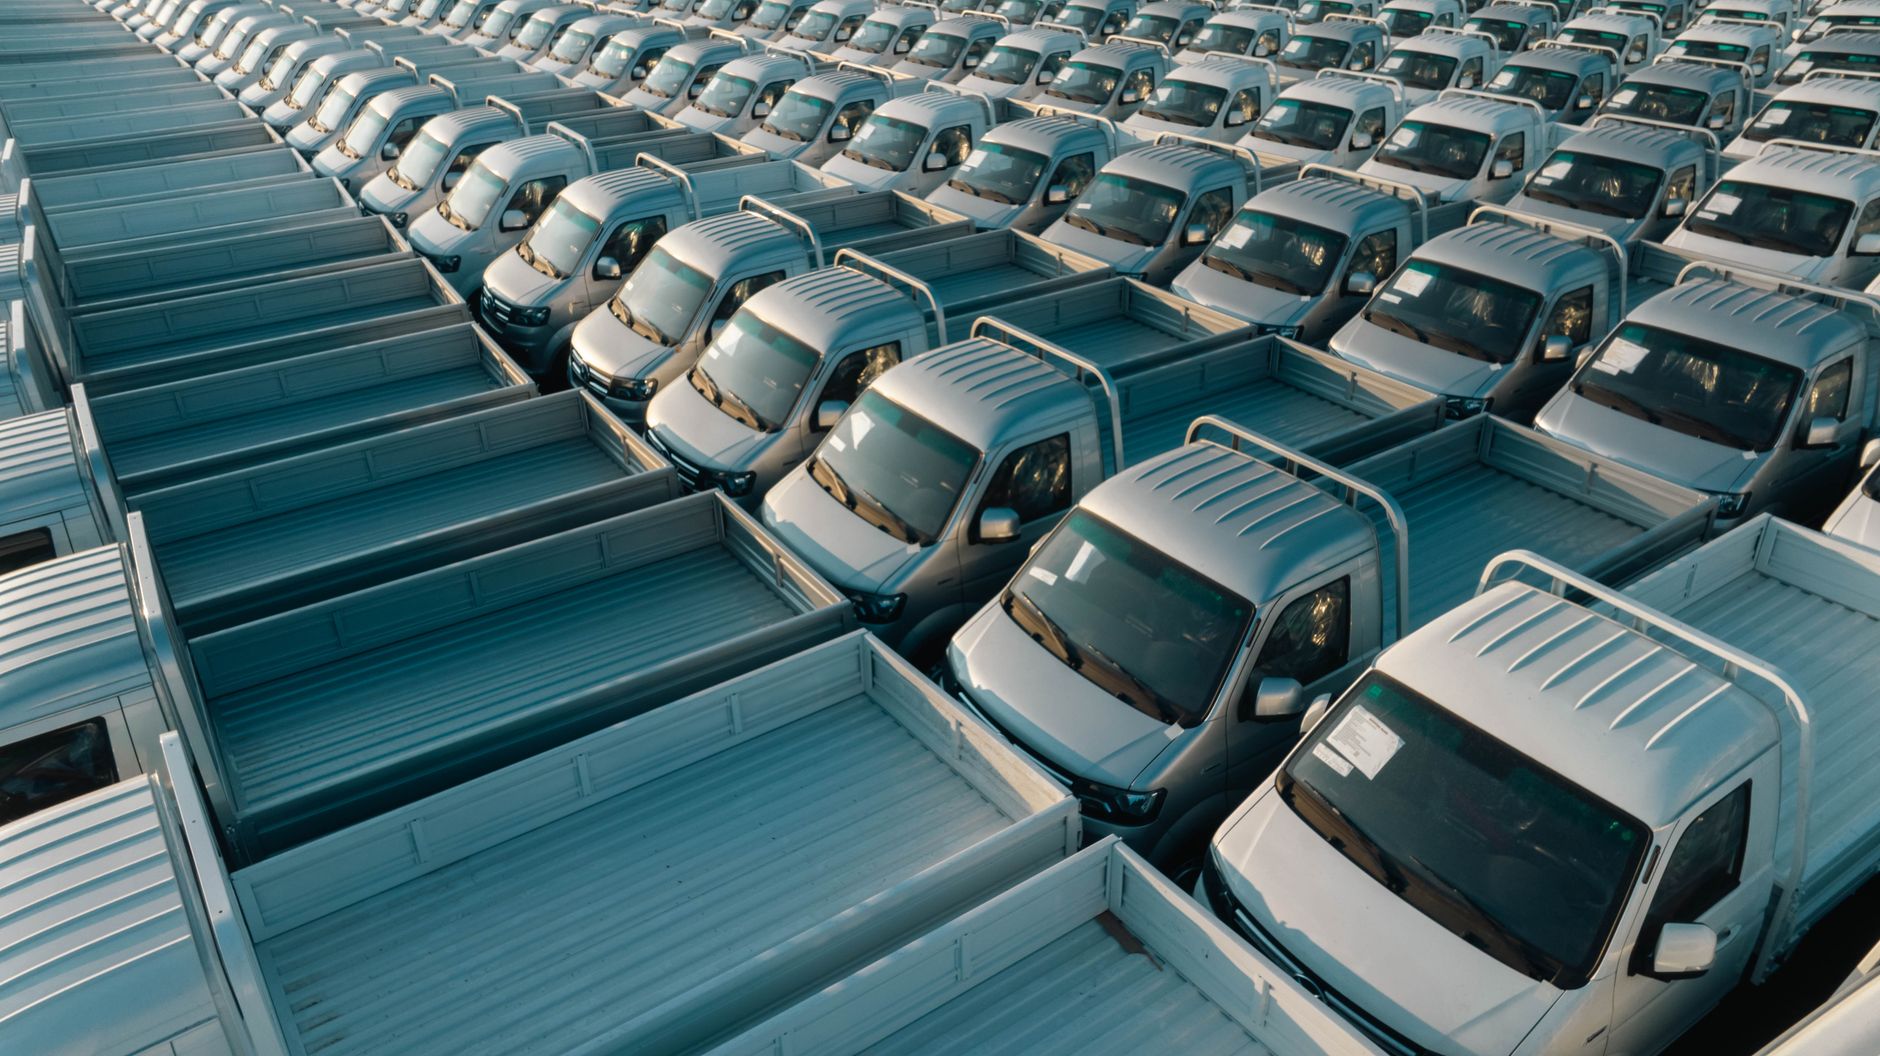
Completed vehicles may move by truck, rail, or ocean vessel to ports, distribution compounds, dealers, and customers. Handling plans must account for capacity, damage prevention, tracking, and delivery appointments. Aftermarket networks instead distribute replacement parts to dealers, workshops, and consumers; their demand patterns and service-level requirements differ from those of assembly plants. Pick, pack, and ship workflows support relevant parts-fulfillment activities.
For recall-related work, vehicle and component identification must be reconciled with the applicable recall instructions. In the United States, NHTSA’s recall lookup allows users to check for open vehicle recalls; it is not a substitute for a manufacturer’s parts-traceability records.
Reverse flows
Reverse logistics covers reusable packaging, warranty returns, defective components, cores for remanufacturing, and materials sent for recycling or disposal. Electric-vehicle batteries require particular attention to condition, packaging, and applicable transport rules. The U.S. Pipeline and Hazardous Materials Safety Administration provides lithium battery transportation guidance.
Technology and Information
A warehouse management system records inventory locations and directs activities such as receiving, put-away, picking, and counting. A transportation management system can support shipment planning and execution, while enterprise and manufacturing systems exchange purchasing and production information. Mobile warehouse workflows and barcode identification can help operators capture transactions at the point of work.
Useful data include part number, quantity, unit of measure, location, supplier, shipment status, and, where required, lot or serial identity. Lot tracking can help businesses trace affected inventory, but effective traceability also depends on supplier records, consistent identifiers, and timely data exchange. RFID, sensors, and predictive analytics may supplement these controls where their benefits justify implementation costs.
Trading partners can use electronic data interchange standards to exchange business messages; automotive networks also use industry-specific message sets promoted through organizations such as AIAG. Before automating an interface, agree on message timing, acknowledgments, exception handling, and ownership of master data. In particular, verify units of measure and conversions: a release expressed in pieces should not be interpreted as the same number of cartons.
Challenges and Risk Management
Automotive networks must manage variant complexity, long supplier chains, border crossings, equipment shortages, and tightly scheduled production. A late or incorrectly sequenced component can interrupt assembly even when other materials are available. Low inventories can expose a plant to disruption, so JIT should be balanced against credible recovery options rather than treated as an instruction to eliminate all buffers. Toyota describes JIT as part of a broader production system.
Electric-vehicle growth introduces additional planning requirements for battery materials, specialized handling, and transport. The IEA’s EV market analysis provides context on the market as of 2024, while PHMSA guidance addresses U.S. lithium battery transport. Requirements vary by jurisdiction, transport mode, battery condition, and classification; operators should verify the rules applicable to each shipment.
For critical parts, a recovery plan can specify a shortage trigger, escalation contacts, available inventory, approved alternative transport, and the decision process for changing production. Test the plan with suppliers rather than assuming an alternative route or source is immediately available. For battery shipments, incorporate the applicable PHMSA transport guidance into the handling and escalation plan.
Best Practices and Performance Measures
- Map the network and dependencies. Identify suppliers, transport lanes, consolidation points, critical parts, and recovery alternatives. Include lower-tier dependencies where information is available.
- Set differentiated inventory policies. Base buffers on demand variability, lead time, disruption risk, and the consequences of a shortage. Verify stock records through cycle counting.
- Synchronize schedules and master data. Agree on part identifiers, units, delivery windows, packaging quantities, and escalation procedures. Test sequencing and exception messages before production changes.
- Protect products and people. Use suitable packaging and handling instructions; inspect vehicles and components for damage. Apply documented dangerous-goods controls where relevant.
- Measure outcomes and investigate exceptions. Common measures include supplier on-time delivery, line stoppage minutes attributable to material shortages, inventory accuracy, freight cost per vehicle or unit, finished-vehicle damage rate, and aftermarket order fill rate. Define each measure consistently before comparing sites or suppliers. Warehouse productivity tracking can support operational measurement, but should be interpreted alongside quality and safety results.
For example, define supplier on-time delivery as deliveries arriving within an agreed window divided by deliveries due in the period. Specify how early arrivals, partial deliveries, and supplier-controlled versus carrier-controlled delays are treated. Pair the result with shortage-related stoppage minutes so a punctuality percentage does not obscure the operational consequence of an exception.